NEWS
Pellet machines strengthen poultry feed production through controlled processing, reliable output, and seamless equipment integration for commercial farms operating year-round.
Efficient pellet production supports automatic feeding lines, organized material flow, and consistent feed handling across poultry houses serving thousands of birds daily.
Commercial pellet mills connect feed preparation with poultry cages, storage systems, conveyors, ventilation, drinking equipment, egg collection, and manure management.
Proper equipment selection considers production scale, feed formulation, electrical planning, maintenance intervals, and future expansion without disrupting existing poultry operations.
Integrated poultry equipment solutions create coordinated farm workflows, combining practical engineering, automated operation, scalable capacity, and global project support for commercial production.
Get professional poultry farm construction guidance, equipment selection solutions, and the latest price lists.
Please contact us, WhatsApp NO. : +8613582487372, click to learn more:
Better Feed Handling
Feed handling becomes more predictable when loose mash is processed into properly formed pellets.
A commercial pellet machine reduces dust during transportation and feeding while allowing automatic equipment to move feed efficiently through pipelines extending 60–180 m and conveyor systems operating at 0.3–0.8 m/s.
This becomes especially valuable when a poultry farm operates multiple houses, long feeding lines, or large-scale layer cage systems.
The result is a feed system designed around continuous production rather than repeated manual handling.
Improved Feeding Efficiency
Feed form directly influences how birds interact with their daily ration.
Data is for reference only.Swipe horizontally to view full table.
A poultry feed pellet mill becomes more than a feed-processing device.
Feed preparation connects with modern poultry production systems operating under feed cycle intervals of 4–8 hours and storage turnover periods of 5–12 days.
When combined with automatic feeders, feed storage bins, conveyors, and poultry cages, such equipment supports a more controlled production workflow.
Lower Feed Waste
Imagine two feeding systems operating beside each other.
One handles loose feed through repeated manual transfer.
The other uses a commercial pellet machine, storage equipment, conveyors, and automatic feeding lines supported by silo capacities of 8–30 tons and distribution accuracy within ±3%.
The second arrangement creates a more organized material flow from raw ingredients to the birds.
Data is for reference only.Swipe horizontally to view full table.
For larger poultry farms, reducing unnecessary feed movement can simplify daily management and support more consistent feeding schedules.
Supports Automated Poultry Farms
Automation is not limited to cages and egg collection.
A complete poultry equipment solution can integrate feed production with storage, conveying, feeding, drinking, ventilation, and environmental control while maintaining feed transport distances of 150–300 m and operating availability above 95%.
Data is for reference only.Swipe horizontally to view full table.
A properly configured poultry feed pellet machine becomes particularly useful for commercial layer farms where thousands of birds must receive feed according to a controlled routine.
Coordinated equipment also reduces dependence on repeated manual operations inside the poultry house.
Fits Large-Scale Farm Expansion
Farm expansion changes the importance of feed-processing capacity.
A small poultry operation may purchase prepared feed from outside suppliers.
A growing commercial operation may eventually need greater control over feed availability, production scheduling, and transportation while managing daily feed consumption between 0.6 and 180 tons and annual production plans exceeding 2,000 tons.
Data is for reference only.Swipe horizontally to view full table.
A commercial pellet mill becomes particularly valuable when a poultry farm is planned as a long-term production project rather than a single-house operation.
Pellet Machines And Feed Mill Planning
A pellet machine should be selected according to the complete feed-production process.
Raw materials require receiving, cleaning, grinding, batching, mixing, conditioning, pelleting, cooling, screening, and storage while maintaining ingredient particle sizes between 0.6 and 1.2 mm and batching tolerances within ±0.5%.
Data is for reference only.Swipe horizontally to view full table.
Planning these stages together helps avoid creating a pellet machine capacity that does not match upstream or downstream equipment.
Pellet Production And Poultry Cage Systems
Feed production becomes more valuable when it directly supports efficient poultry housing.
For layer farms, automatic H-type cage systems can accommodate large bird populations while integrating feeding, drinking, egg collection, and manure management, with feed trough depths of 90–150 mm and feed line service lengths reaching 120 m.
Data is for reference only.Swipe horizontally to view full table.
A poultry feed pellet machine should therefore be considered together with cage layout, house dimensions, bird capacity, and automation level.
Integrated equipment planning allows feed delivery to match the physical arrangement of commercial poultry houses.
Why Equipment Integration Matters
Think of the farm as one connected production chain.
Feed ingredients enter the processing area.
Pellets move into storage.
Conveyors deliver feed toward each poultry house through transfer systems covering 100–250 m and control networks responding within 0.2–1.0 seconds.
Automatic feeders distribute the ration.
Birds remain within organized cage environments while other systems manage water, eggs, ventilation, and manure.
Data is for reference only.Swipe horizontally to view full table.
This structure allows equipment suppliers to design the poultry farm around production capacity instead of treating each machine as an isolated purchase.
Choosing A Pellet Machine For Commercial Use
The right machine depends on feed volume, bird population, formula requirements, available power, and the planned automation level.
A commercial project should also consider spare parts, motor configuration, maintenance access, cooling capacity, and future expansion while targeting maintenance intervals of 800–2,000 hours and bearing service lives exceeding 20,000 hours.
Data is for reference only.Swipe horizontally to view full table.
Selecting equipment from the beginning of the farm design can make later integration considerably easier.
Building A More Complete Poultry Production System
The five reasons are ultimately connected pellet machines improve feed processing, simplify handling, support automation, reduce unnecessary feed movement, and provide a scalable foundation for expanding poultry production.
When feed equipment is planned together with poultry cage systems and other poultry farm equipment, the entire farm can operate as a coordinated production system supported by electrical loads ranging from 80–600 kw and operational utilization rates of 85–98%.
For farms seeking a complete equipment solution, hb best provides poultry cages, automatic feeding systems, drinking systems, egg collection equipment, manure removal systems, ventilation equipment, and turnkey poultry farm engineering.
The goal is not simply to supply one pellet machine.
It is to help build a practical poultry production system that matches bird capacity, house design, automation requirements, and future farm expansion.
Frequently Asked Questions
Q1: What does a pellet machine do for a poultry farm?
A1: A pellet machine processes formulated feed into uniform pellets for easier storage, transport, and automated distribution.
Commercial systems can operate within production lines designed around continuous daily feed requirements.
Q2: How should a pellet machine be integrated with poultry equipment?
A2: Feed processing should connect with silos, conveyors, automatic feeders, poultry cages, and control systems.
Integration should also consider house layout, electrical capacity, and planned expansion before installation.
Q3: Is a pellet machine suitable for large commercial poultry projects?
A3: Yes.
A properly selected poultry feed pellet machine can support expanding operations when production capacity, storage, feeding routes, and downstream equipment are engineered together.
Taiyu (HK) Group - One Of China Toppest Pellet Machine Manufacturer
Pellet machines provide controlled feed processing with integrated conditioning, compression, cooling, and material-transfer architecture for commercial poultry production.
Global factory direct sales provide coordinated poultry equipment supply, technical documentation, component matching, and project-based equipment configuration.
Turn-key poultry engineering covers poultry cages, automatic feeding, drinking, ventilation, egg collection, manure removal, and complete house equipment integration.
Project support covers farm layouts from individual poultry houses to large commercial facilities, with equipment selection aligned to bird capacity and production objectives.
Engineering teams coordinate equipment interfaces, installation requirements, commissioning procedures, spare parts planning, and operational support for international poultry farm projects.
Contact Us To Received Your Customized Poultry Farm Plan
Headquarters And Branchs
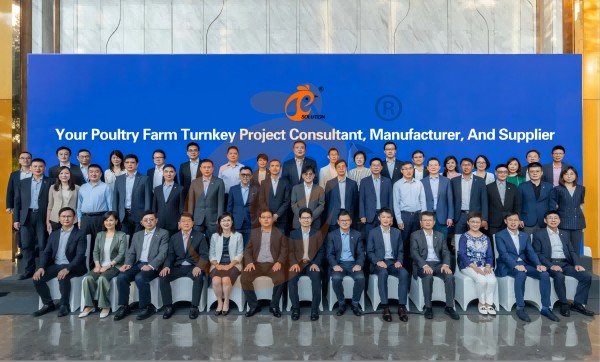
Hong Kong Headquarter Management Team
Hong Kong Headquarter Taiyu Industrial Group CO., LTD
China Hebei Best Machinery And Equipment CO., LTD
Nigeria Vanke Machinery And Equipment CO., LTD
Tanzania Best Machinery And Equipment CO., LTD
Ethiopia Best Hebei Machinery Manufacturing PLC
Reception /24 online WhatsApp NO. : +8613582487372
Share


More
 Layer Chicken Cage Management | 7 Key Tips For Higher Egg Yield
- 6 Practical Ways To Reduce Water Waste With Nipple Drinkers
- How To Reduce Feed Waste With Pralson Feeders | 5 Effective Methods
 How To Reduce Feed Waste With Pellet Machines | 5 Effective Ways
- Deep Litter System Biosecurity | 5 Essential Protection Measures
- 6 Practical Ways To Improve Feeding In Broiler Chicken Cages
- Why Nipple Drinkers Are Important | 5 Proven Benefits For Poultry
- 6 Practical Steps To Optimize Pralson Feeder Performance